2026 Best Dual Torch Pipeline Welding Machine?
Choosing the 2026 Best Dual Torch Pipeline Welding Machine requires more than comparing power ratings and advertised production speeds. Pipeline welding involves long shifts, uneven ground, changing weather, and demanding joint consistency. A capable Dual Torch Pipeline Welding Machine should support stable arc performance, accurate torch alignment, controlled heat input, and practical adjustment during field work. Fit matters.
This guide examines the features that influence real welding results. We will consider welding capacity, torch synchronization, fuel or power requirements, control systems, portability, maintenance access, and operator visibility. A machine may look impressive on a specification sheet, yet perform poorly when cables are difficult to manage or controls become unreliable under dust and vibration. That gap matters. Experience from fabrication and pipeline environments shows that small design details often affect productivity more than headline output.
No single machine is perfect for every crew, pipe diameter, or project schedule. I would not rank equipment using marketing claims alone. Independent test data, manufacturer documentation, warranty support, replacement-part availability, and recognized safety certifications deserve equal attention. Buyers should also verify compatibility with their welding process, consumables, and site procedures. Some recommendations may appear less powerful, but they can offer better control and lower downtime. That is not always obvious. This review aims to separate useful engineering from attractive wording, while acknowledging that field conditions can expose weaknesses that laboratory testing misses. The final choice should balance performance, reliability, operator comfort, and long-term service value.
What Is a Dual Torch Pipeline Welding Machine?
2026 Best Dual Torch Pipeline Welding Machine?
What Is a Dual Torch Pipeline Welding Machine?
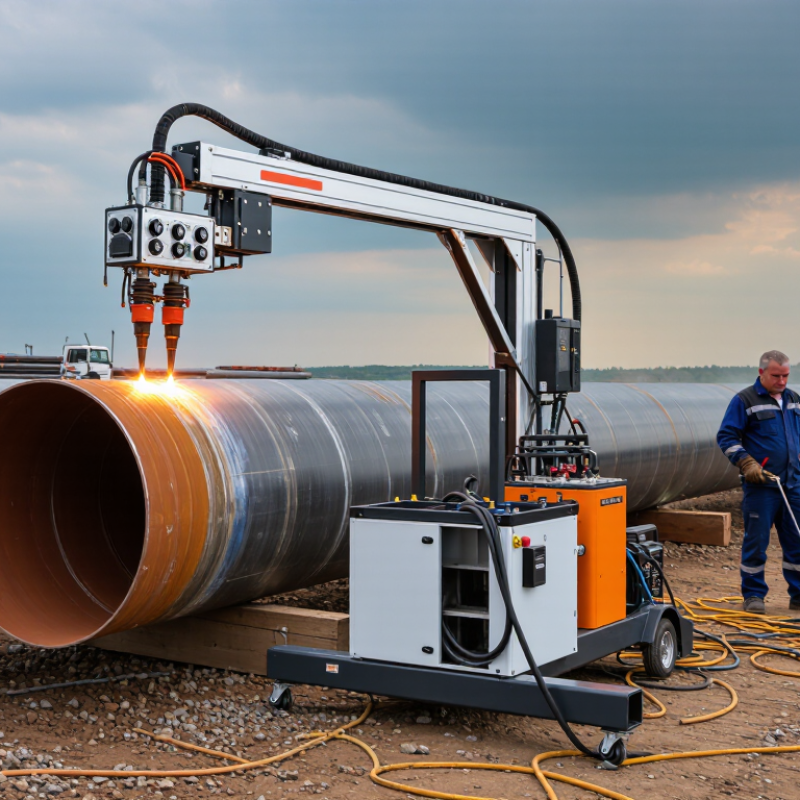
A dual torch pipeline welding machine uses two welding torches during one pipe joining operation. One torch may weld the root area, while the second follows for filling or finishing. This arrangement can improve production speed and maintain steadier heat distribution on large-diameter pipelines.
The machine usually includes synchronized controls, adjustable travel speed, torch holders, and a powered carriage. Operators can set welding current, voltage, wire speed, and torch spacing for each joint. In field work, alignment matters greatly. A small mismatch can create uneven penetration, excessive reinforcement, or visible undercutting. Clean preparation is essential.
Real-world performance depends on pipe thickness, joint design, welding process, and site conditions. Wind, moisture, poor grounding, or unstable power can reduce weld quality. Experienced technicians inspect the root bead before allowing later passes to continue. They also verify settings against approved welding procedures and applicable safety requirements. That check takes time.
It is not automatic perfection.
A dual torch system can reduce labor and improve consistency, but it still requires trained supervision. Some applications may benefit from two torches, while narrow spaces may make one torch more practical. I have found that advertised speed is only part of the decision. Maintenance access, spare components, control response, and operator training often determine whether the equipment performs reliably over many shifts.
How Dual Torch Welding Technology Works
2026 Best Dual Torch Pipeline Welding Machine?
How Dual Torch Welding Technology Works
Dual torch welding technology uses two coordinated heat sources on one pipe joint. One torch leads, while the second follows at a controlled distance. The leading torch begins penetration. The trailing torch refines the bead and balances heat across the seam. This arrangement can reduce repeated passes on suitable pipeline materials.
The system usually combines torch positioning, travel speed, current, and gas flow controls. Some machines use sensors to track the joint as the pipe rotates. Others depend more heavily on operator adjustments. In field work, alignment matters as much as power. A small offset can create uneven fusion, excessive reinforcement, or local overheating.
Temperature control remains critical. Too little heat leaves incomplete penetration. Too much heat may distort the pipe or weaken the heat-affected zone. Experienced technicians check bead shape, arc stability, and interpass temperature throughout the weld. They also verify calibration before production begins.
It is not foolproof.
Dual torches can improve productivity, but they also increase setup complexity. I have found that rushed synchronization causes more problems than slower, careful preparation. Pipe diameter, wall thickness, joint design, and material grade must guide the settings. A machine that performs well on thick carbon steel may behave differently on stainless alloys. Trial welds and qualified inspection remain necessary, even when the control system appears reliable.
2026 Best Dual Torch Pipeline Welding Machine? — How Dual Torch Welding Technology Works
A dual-torch pipeline welding system uses two independently controlled arcs in sequence. The leading torch typically provides preheating and filler-metal deposition, while the trailing torch completes fusion, shaping, or cap-pass work. The chart shows representative electrical input calculated from current × voltage; actual settings depend on pipe material, wall thickness, wire, shielding gas, and welding procedure qualification.
Representative operating values: Torch 1 at 180 A and 24 V = 4.32 kW; Torch 2 at 220 A and 26 V = 5.72 kW. Electrical input is calculated, not a brand-specific performance claim.
Safety and Operating Procedures
A dual-torch pipeline welding machine demands disciplined preparation, not confident guesswork. Before work, I inspect torch bodies, hoses, regulators, flashback protection, and ground connections for damage. Cylinders must stand upright, secured, and away from heat. I verify gas labels and test connections with approved leak-detection fluid. Never use a flame for testing. Ventilation matters, even outdoors, because trenches can trap fumes and fuel gas. The work zone stays clear of oil, loose rags, and combustible coatings. Good preparation feels slow. It prevents hurried decisions later.
Operators should wear a correctly shaded helmet, flame-resistant clothing, leather gloves, safety boots, and hearing protection when required. Screens protect nearby workers from sparks and intense light. I confirm the machine’s rated capacity and follow its current operating manual. Pressure and flow settings should match the procedure, material, torch size, and weather. Two torches require clear communication. One person should direct starts, stops, and adjustments. Before ignition, open valves gradually, purge lines safely, and use the approved igniter. Never light gas near a suspected leak. That sounds obvious. It still gets overlooked.
During welding, keep hoses away from hot pipe edges and moving equipment. Watch both torches, puddles, gauges, and nearby personnel without leaning into the heat. If a flame flashes back, a hose heats unexpectedly, or gas odor appears, stop and isolate supplies. Do not restart until the cause is identified. After welding, close cylinder valves, release line pressure, switch off power, and mark hot metal clearly. A fire watch should remain until sparks and heat no longer threaten the area. My weak point is assuming familiar equipment is safe. I now pause and recheck it.
Maintenance, Applications, and Future Developments
A dual torch pipeline welding machine can raise productivity by welding two seams or heating zones in controlled sequence. Its value depends on maintenance, not speed alone. Before each shift, inspect torch alignment, cable insulation, gas hoses, cooling lines, and emergency stops. Small leaks can disturb shielding and create porous welds. Clean contact surfaces daily, and record voltage, travel speed, gas flow, and wire condition.
Applications vary across long pipeline sections, fabrication yards, and repair stations. Dual torches can reduce heat concentration and improve production consistency when operators balance their settings carefully. However, uneven torch angles may produce undercutting or excessive heat input. I have seen experienced teams overlook this during long shifts. The machine still needs qualified supervision, approved welding procedures, and inspection records. Automation helps, but it does not replace judgment.
Tips: Calibrate sensors before critical work. Keep spare liners and contact tips nearby. Test cooling flow before starting. Review weld profiles after the first joint, not after ten. Future models may use thermal cameras, adaptive arc control, and predictive maintenance software. These systems could adjust travel speed as joint gaps change. Energy-efficient power modules may also reduce operating costs. Yet digital warnings can be missed, especially in noisy workshops. A simple visual inspection remains useful.